
Publication archive
Automatic buckle assembly for sandals
Insight into a published application or lecture from the CRETEC archive.
Archive content: Information refers to the original publication status. Please coordinate current execution, scope of services and availability with CRETEC.
 Enlarge the image ↗
 Enlarge the image ↗
 Enlarge the image ↗
 Enlarge the image ↗
 Enlarge the image ↗
 Enlarge the image ↗
 Enlarge the image ↗
 Enlarge the image ↗
 Enlarge the image ↗
 Enlarge the image ↗
 Enlarge the image ↗
 Enlarge the image ↗
 Enlarge the image ↗
 Enlarge the image ↗
 Enlarge the image ↗
Automatic buckle assembly for sandals
Project type:
Automatisation
Date
2019
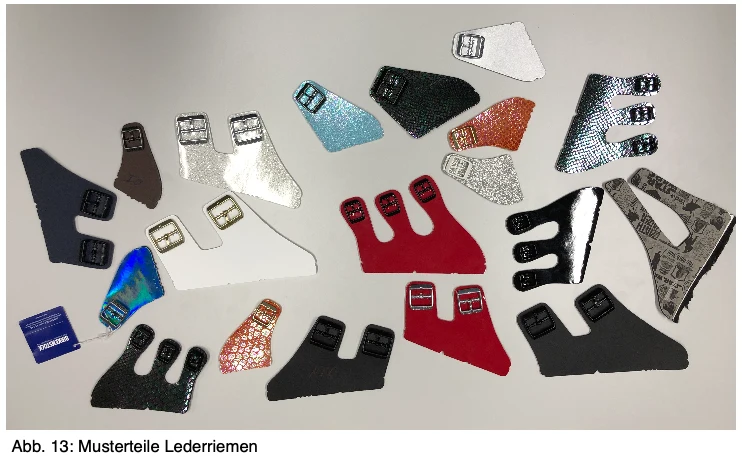
The customer designs a fully automatic series machine that produces the semi-finished product “Sandalen Lederbelmen mit Klammer”.
Several robots and image processing systems are provided in the machine.
The image processing is to be used at 3 stations.
Station 1: Position recognition of the clamps
Station 2: Leather strap position detection
Station 3: Quality control of the semi-finished product
A prototype has already been built. This is now to be optimized.
+ The clamp feeder can be changed
+ The clamp station is provided by the supplier and thus cannot be changed
shall be:
+ All three image processing stations can be projected completely freely.
+ There are no specifications according to the inspection system (Matrix/Linescan/2,5D/3D, etc.) + There is no manufacturer specification
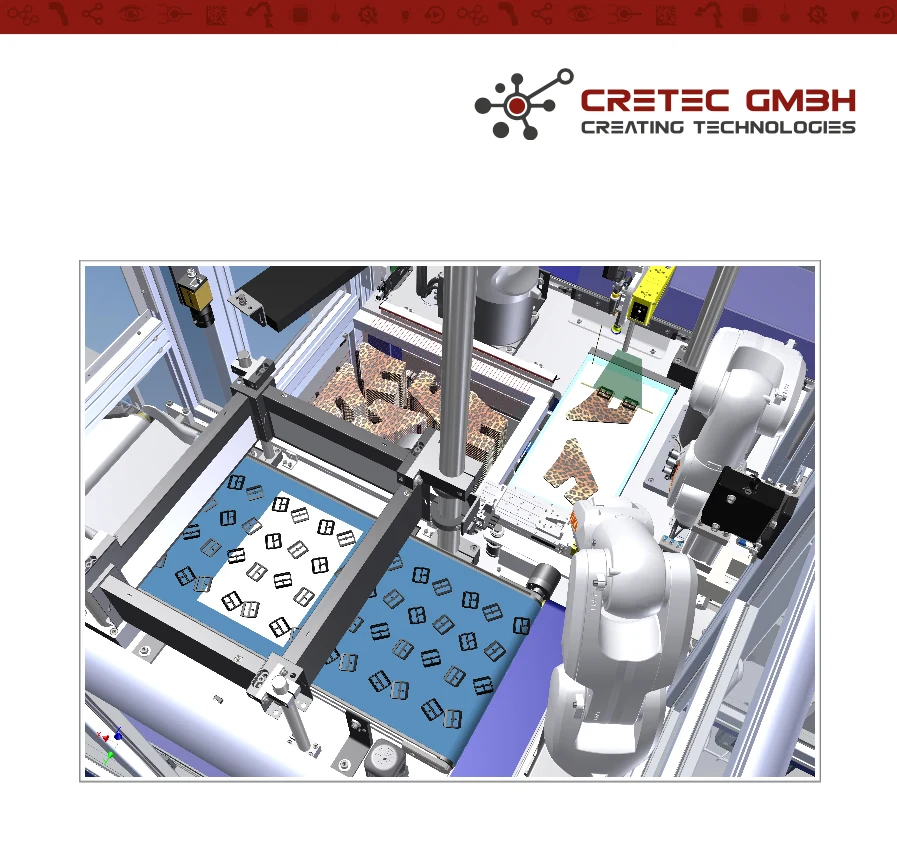
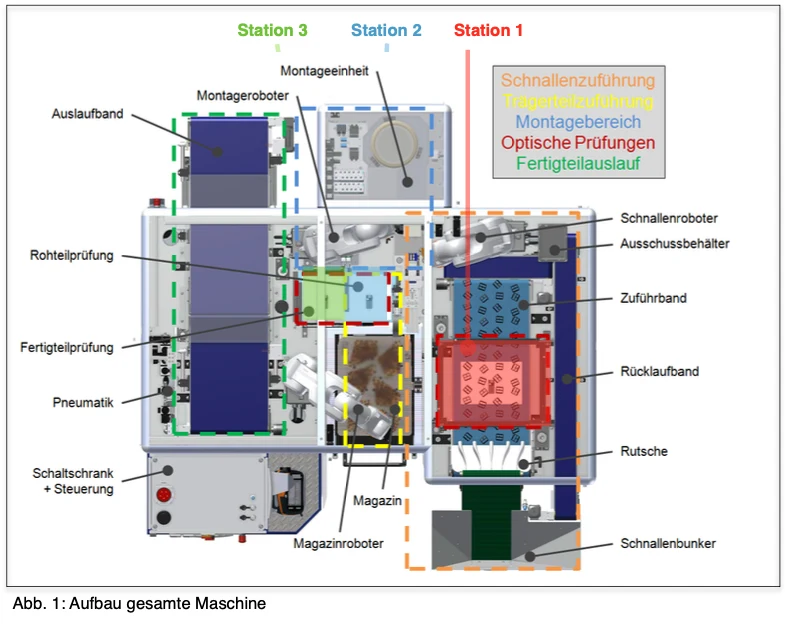
Fig. Fig. 1: Construction of the entire machine
Station 3 Station 2 Station 1
Station 1: Position recognition of the clamps
Instantaneous mechanical structure:
+ The brackets are transported from a bunker to the belt
+ The brackets are usually isolated
+ The brackets are supplied in a single type
It may happen that a false bracket is mixed in.
It may happen that defective brackets are included, in which
For example, the middle hook is missing
+ The tape has a width of 400mm
+ In the prototype, a backlighting of 300 mm is installed
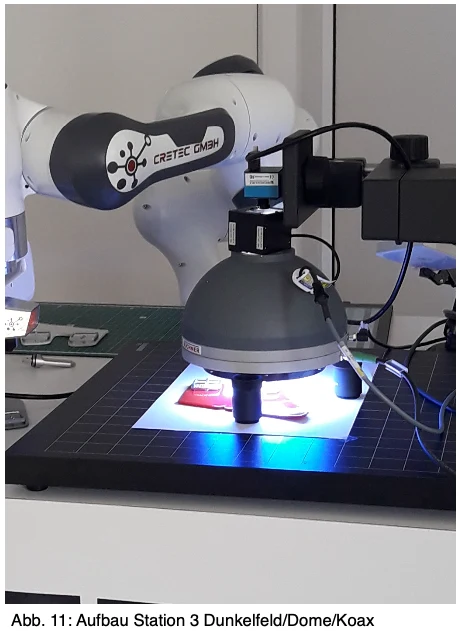
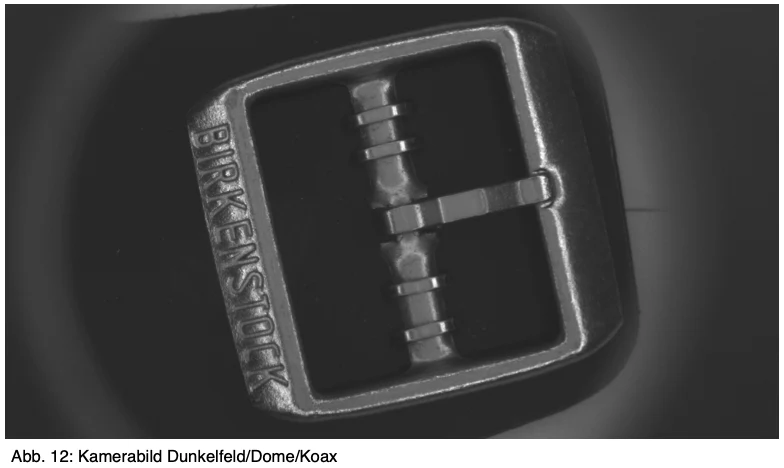
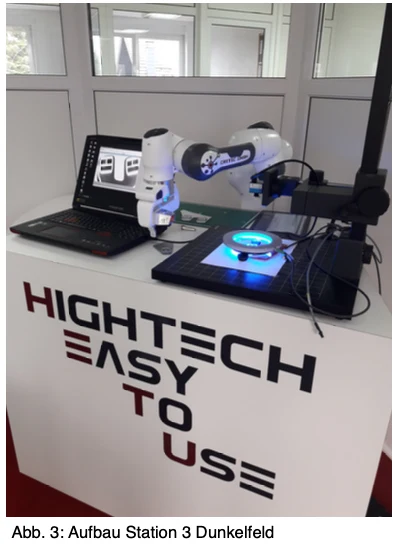
+ In the prototype, there is additionally a square dark field illumination around the image field
Built around
+ In the prototype, the camera looks 90° from above at the backlight and searches for the
Brace contours
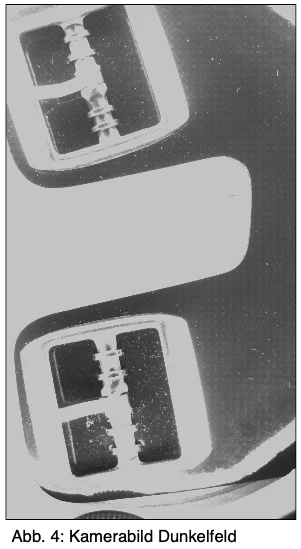
+ In the dark field, the camera searches for the lettering
Problems with prototype:
- at approx. 0.5% of the tests, a bracket lying incorrectly is recognized as being lying around correctly and thus in general. The clamp is then mounted by the robot. The semi-finished product is therefore scrap.
- There will be too few i.O. brackets recognized as such. The image field is thus unnecessarily often cleared and re-equipped. As a result, the required clock rate is not achieved.
Requirements Station 1:
+ Position detection of the clamps to 0.1 mm accuracy (x/y + rotation) + position detection of the clips ( upward or downward font)
+ Clock rate below 0.5 seconds per bracket
+ Sorting out incorrect and defective brackets
Station 2: Position detection of the leather straps
Instantaneous mechanical structure:
+ The leather strap is gripped by the robot and placed on a backlighting
+ The camera looks 90° from above at the backlight
+ The image field is approx. 230 mm x 230 mm
+ The camera searches for the leather contour and passes the x/y + rotation data to the
Robotics
+ The desired contour is given to the system from the CAD data
+ The leather straps are supplied with pure variety (leather type and shoe size always the same)
Problems with prototype:
- When the leather straps are cut from the roll end, they are relatively strongly curved. They then do not lie flat on the backlight. As a result, the camera cannot recognize the position as accurately as required.
Requirements Station 2:
+ Position detection of the leather straps to an accuracy of 0.1 mm (x/y + rotation) + cycle rate below 0.5 seconds per leather belt
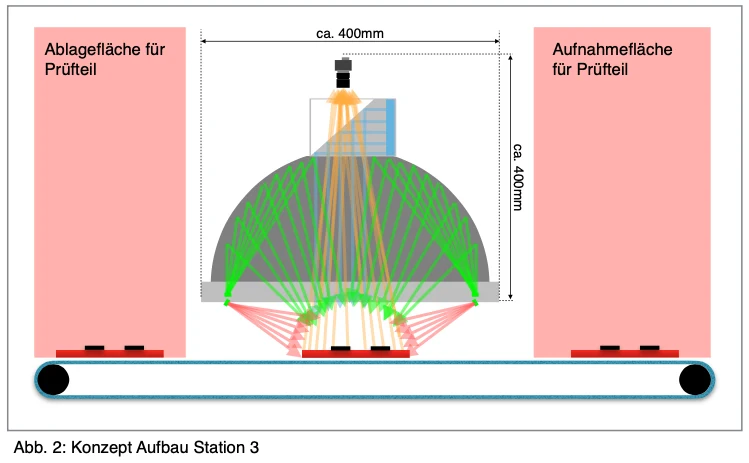
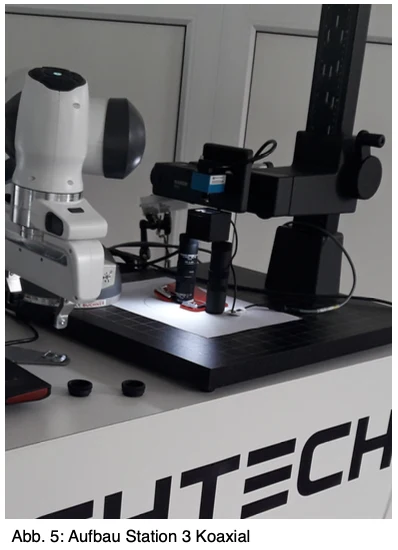
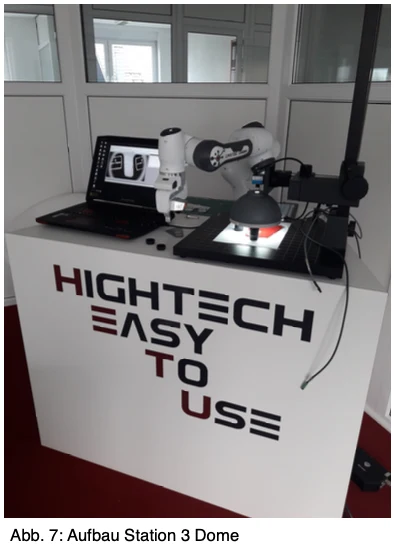
Station 3: Quality control of the semi-finished product
Instantaneous mechanical structure:
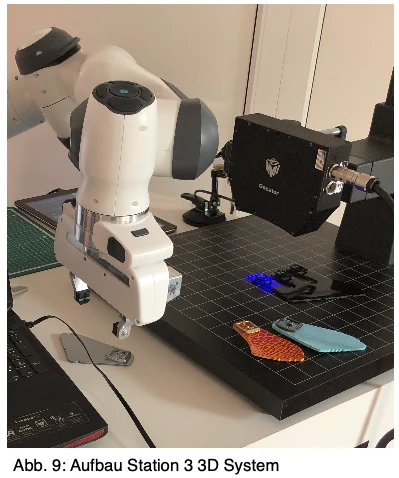
+ The leather strap is removed from the clamp station by the robot and placed on a
Place of test
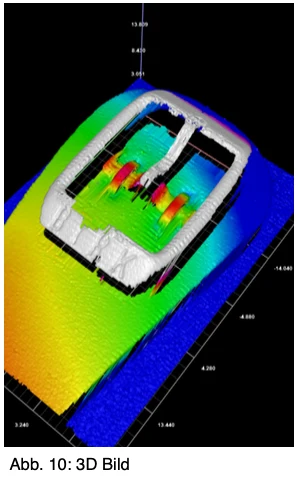
+ Another robot guides a 3D laser line system over the mounted buckles
+field width instantaneously approx. 40 mm
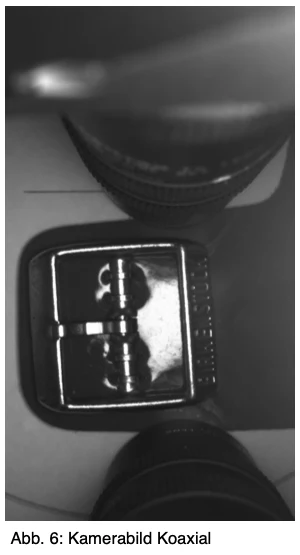
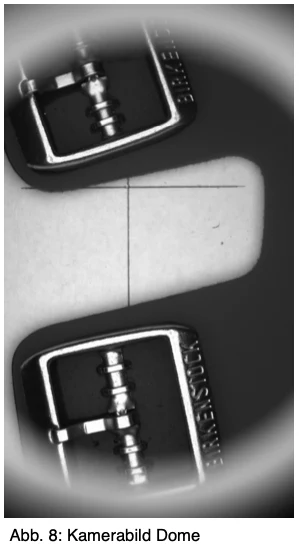
+ The positions of the buckles are checked for the following characteristics:
Presence of the buckle
Correct position of the buckle (upward script)
Presence of brackets
Positions of brackets
+ The semi-finished products are produced in pure variety
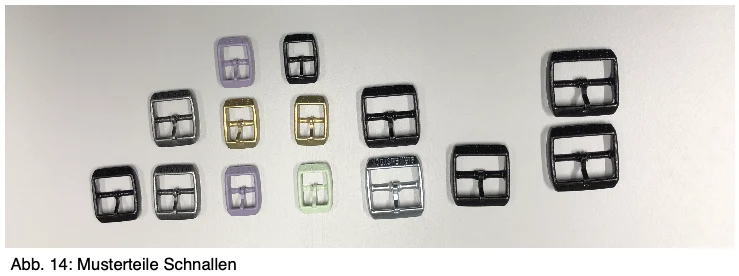
+ Buckles can be used in all conceivable colors
+ brackets can be silver or black
+ Leather can be used in all possible colors
Problems with prototype:
- Examination of black brackets takes too long
- Due to the too slow testing, the cycle rate of the complete system goes down - The angle of the buckles should be in relation to the lowest edge of the semi-finished product
are controlled. This is not possible with the current image field.
Requirements Station 3:
+ Increase clock speed
+ Decrease pseudo-committee
Request for this application →